Prepared Cast Aluminum Parts Application
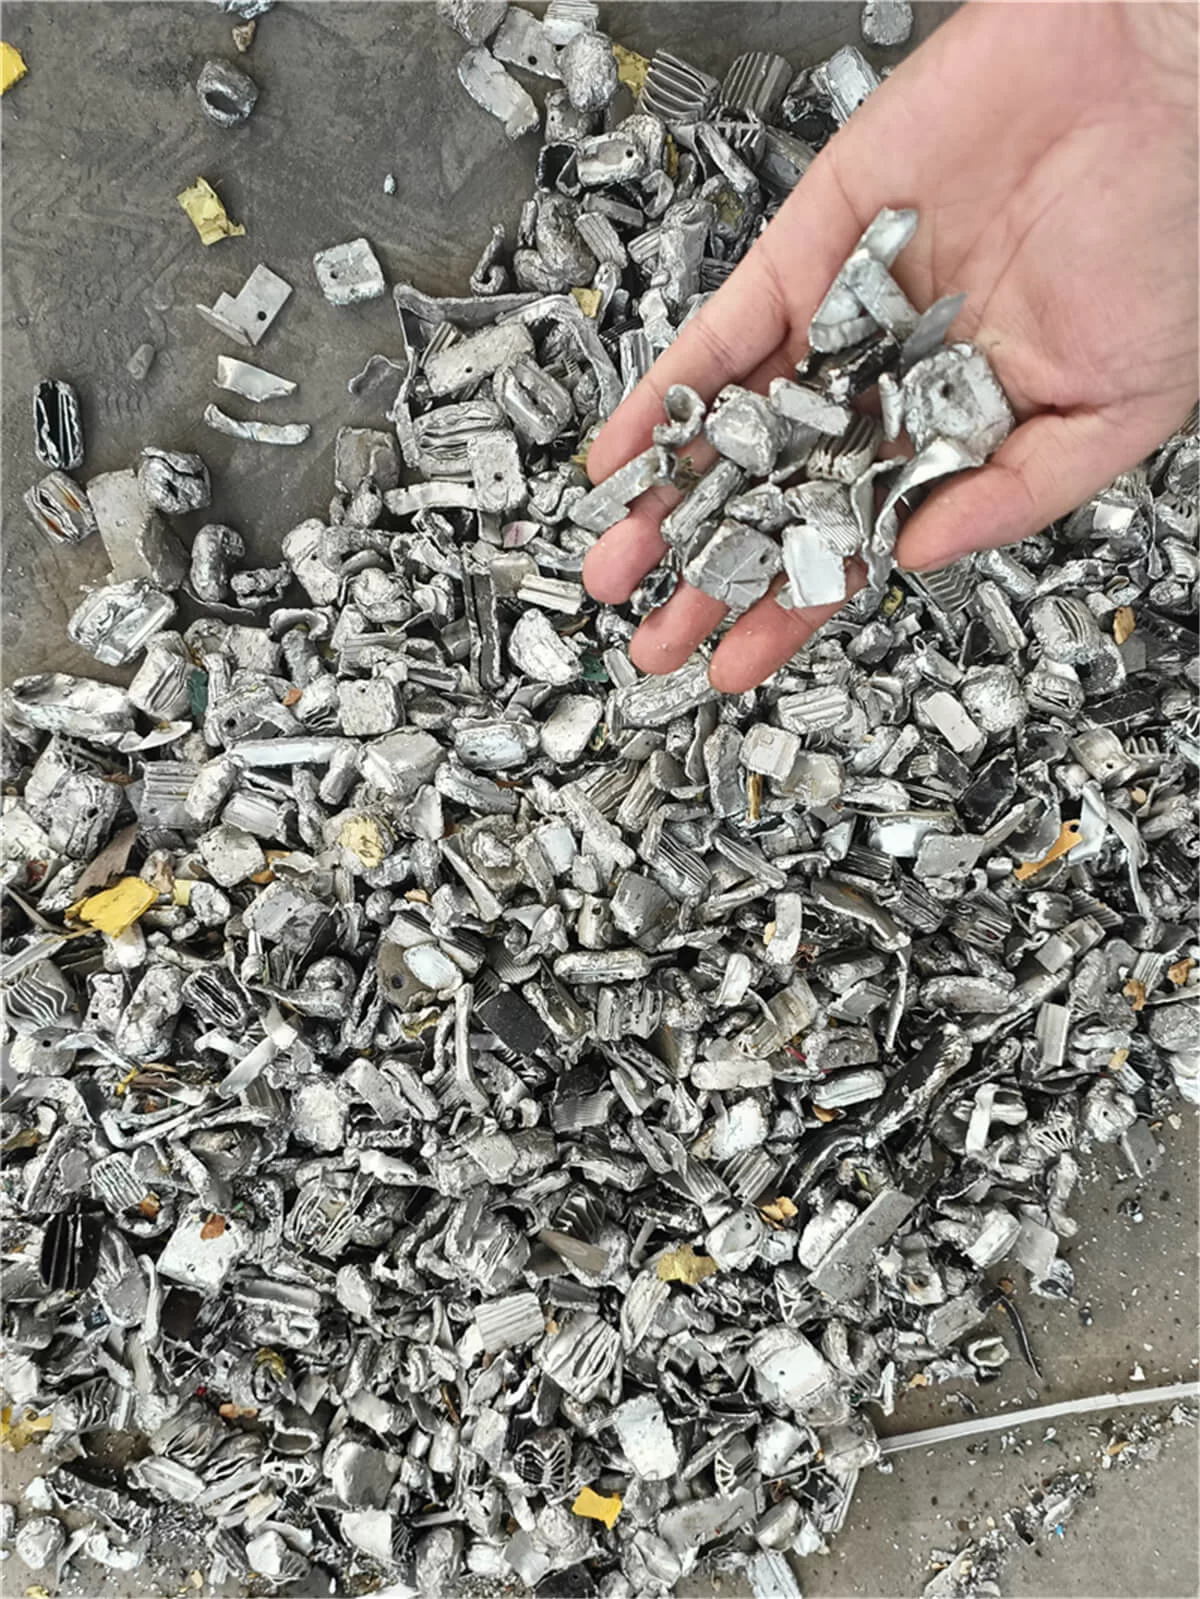
This page focuses on a controlled feed stream of prepared cast aluminum parts such as housings, covers and similar components with known maximum dimensions and wall thickness. It is not intended to represent unsorted mixed casting scrap.
Feed Consistency and Steel Inserts
Stable feeding is easier when part size and composition remain within a defined range. Shafts, bearings, bolts and oversized steel inserts should be identified before crushing. The required downstream magnetic separation depends on how fully the steel and aluminum are liberated.
Selection Data
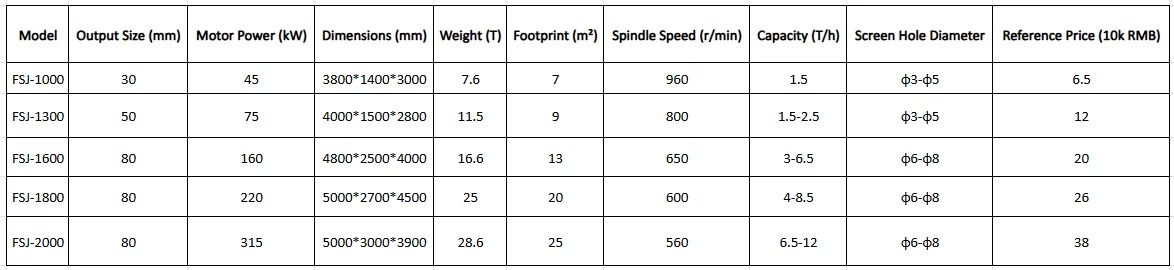
Provide part photos, maximum length, maximum wall thickness, individual weight, percentage of steel attachments, required capacity and target particle size. These conditions determine whether direct crushing is suitable or whether dismantling and pre-treatment are required.
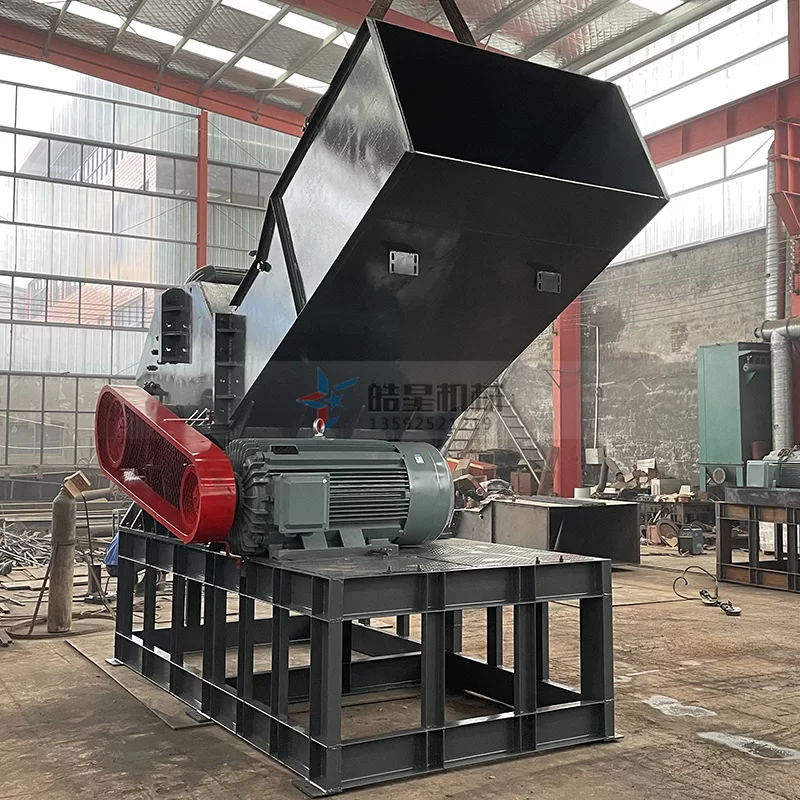
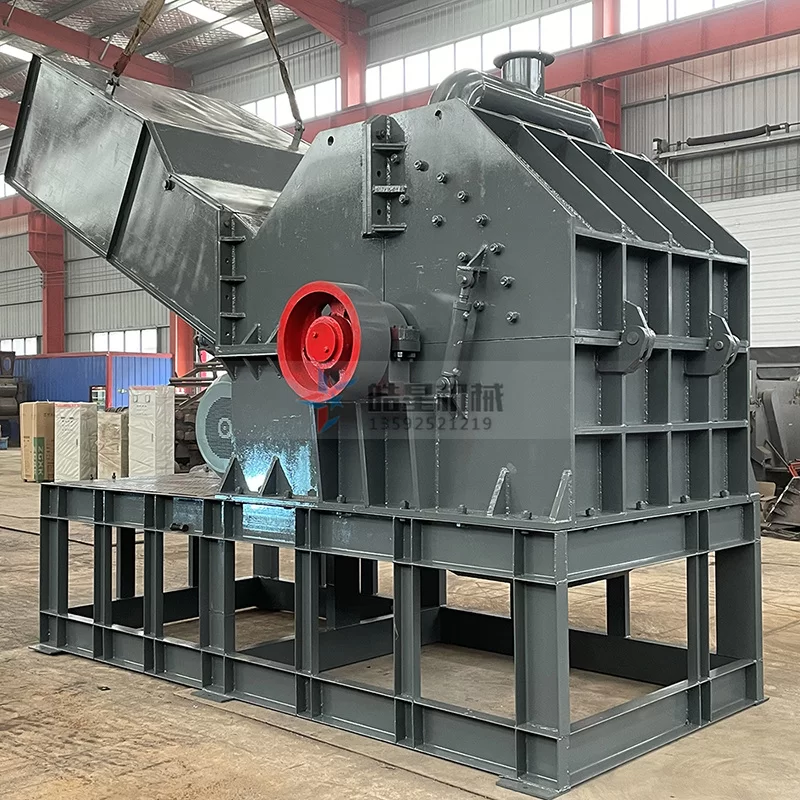
Cast Aluminum Parts Crusher
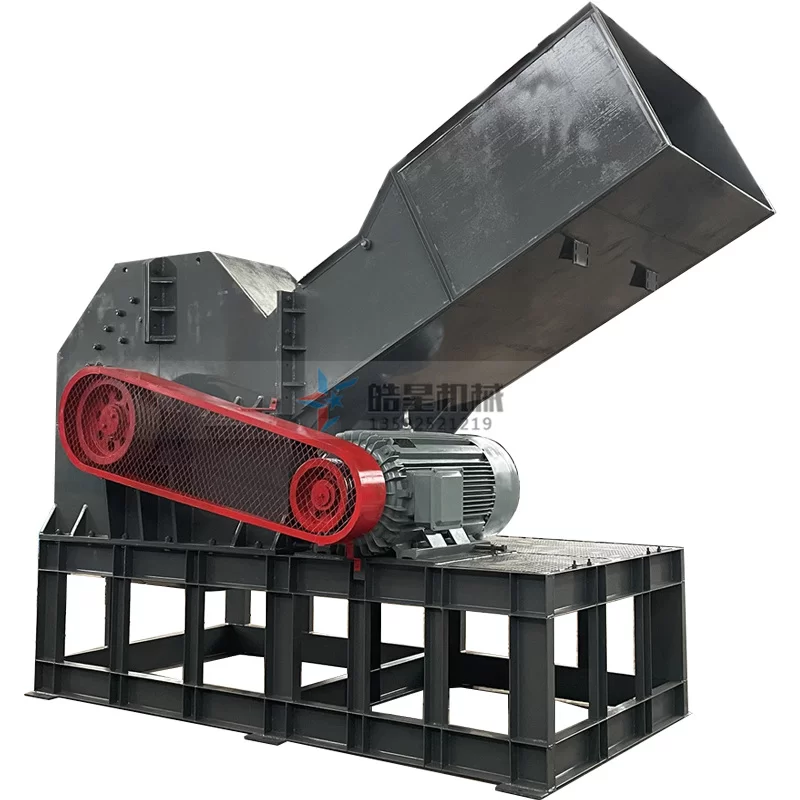
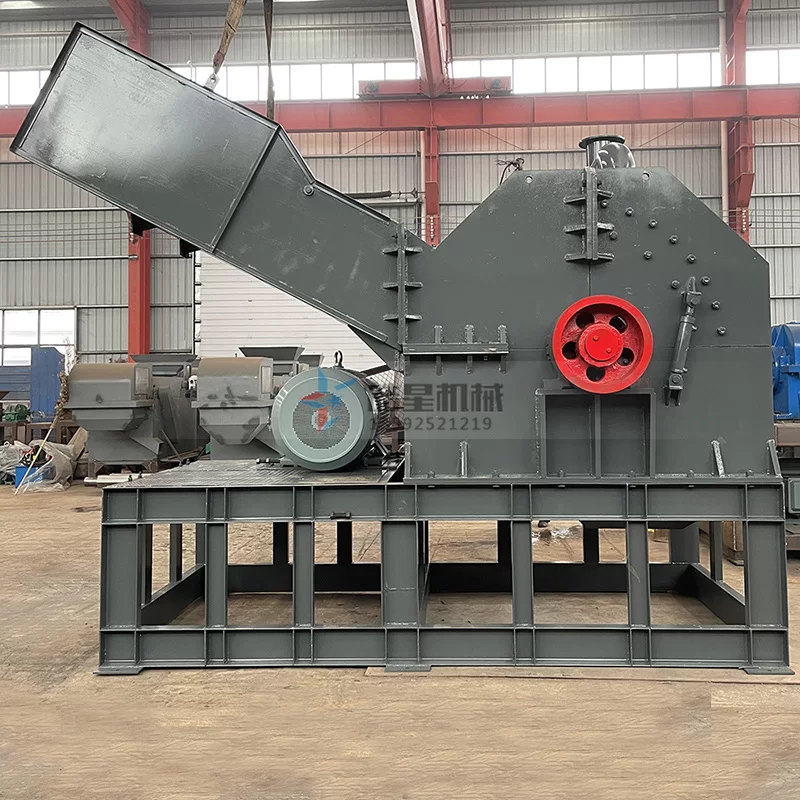
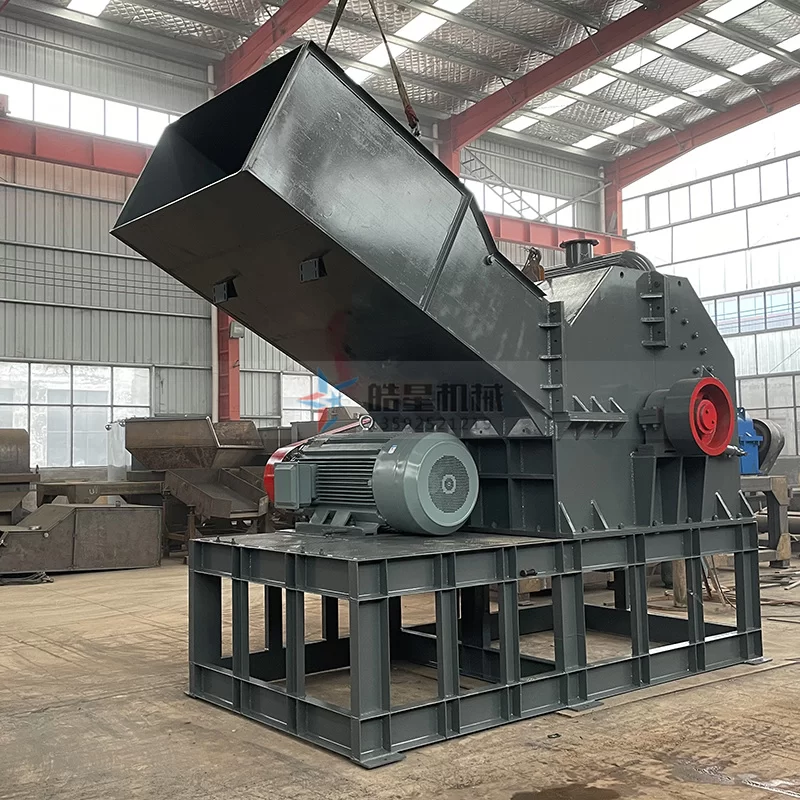
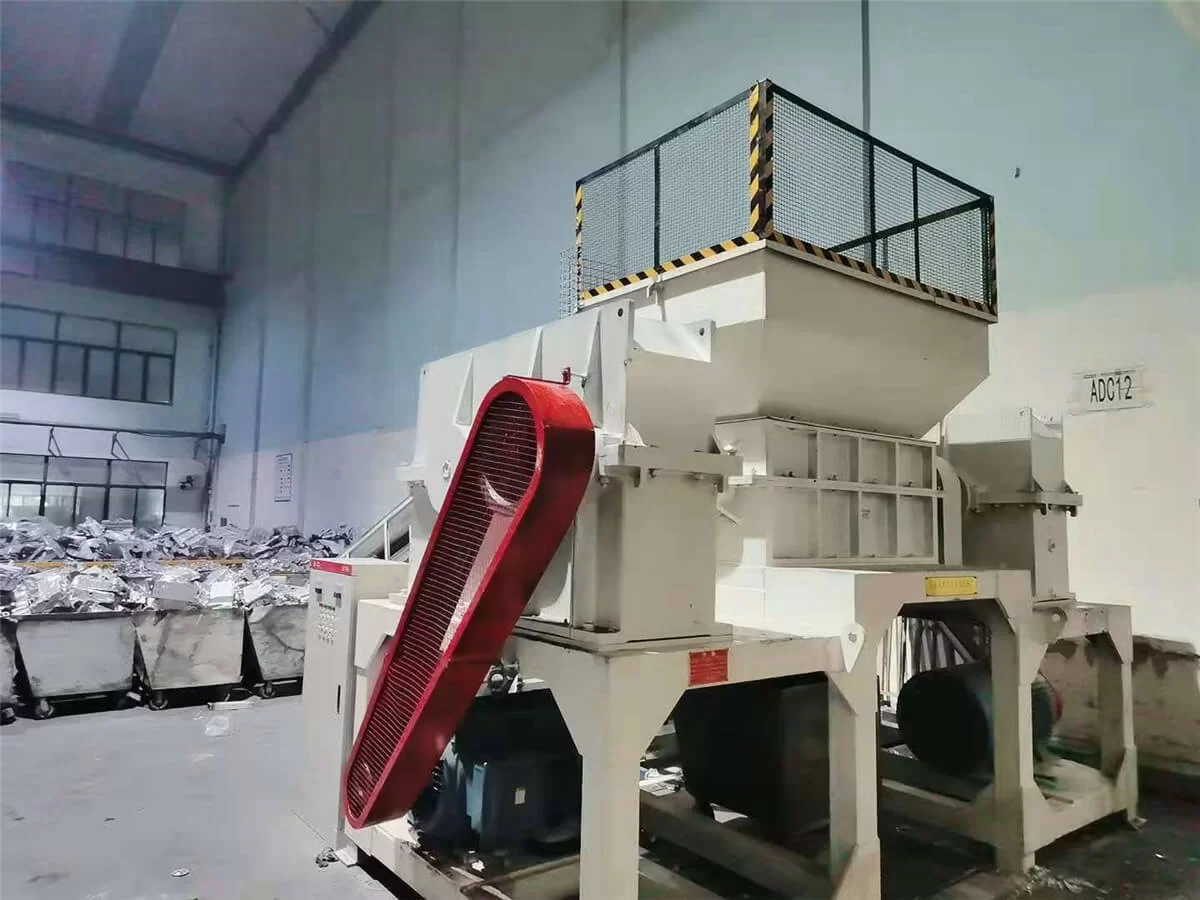
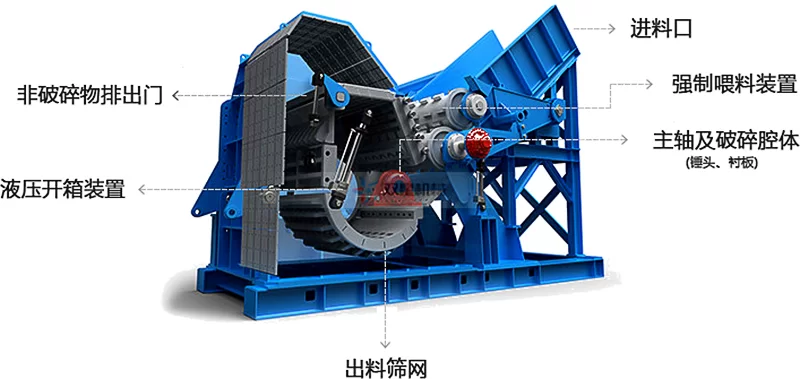
The cast aluminum parts crusher is a high-speed hammer crushing machine designed for prepared cast aluminum components, dismantled housings, rejected die-cast parts and broken aluminum castings.
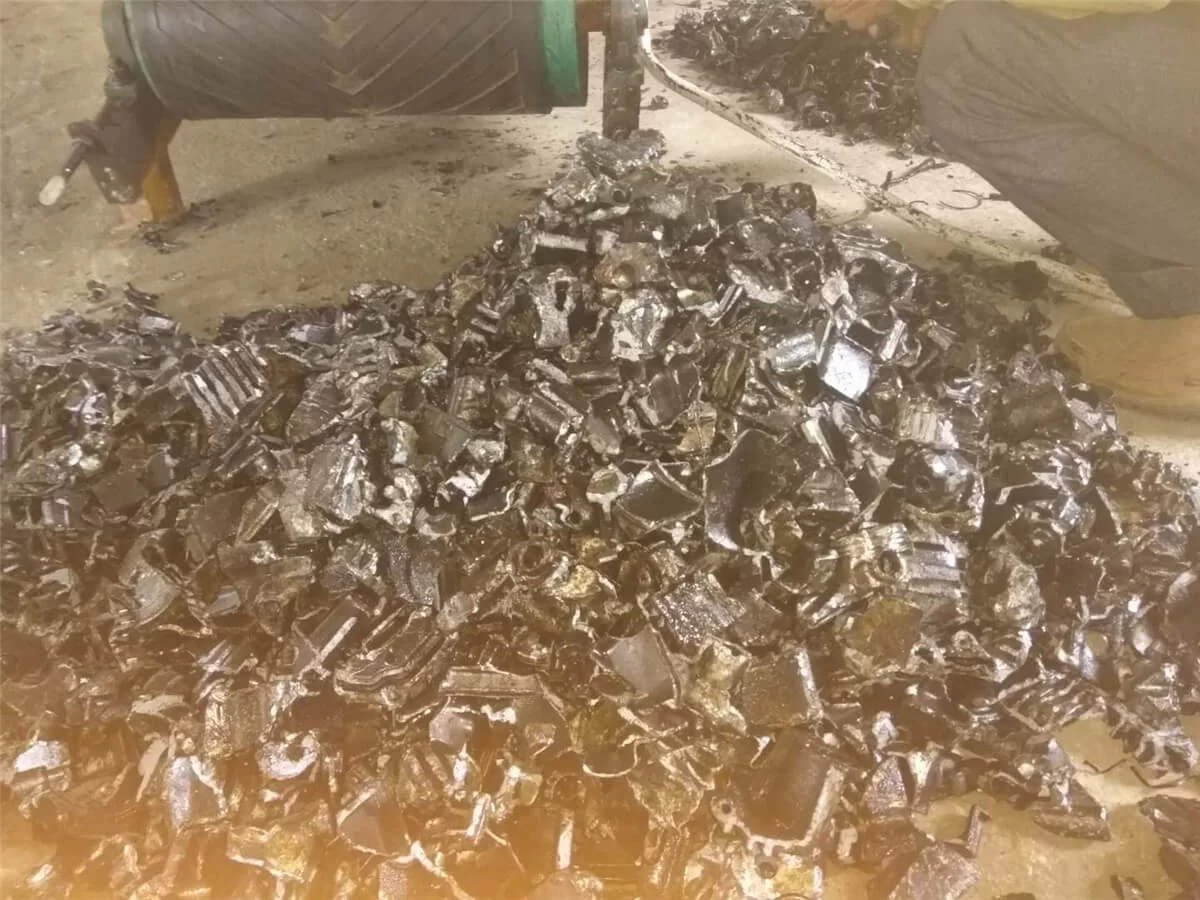
The machine uses a high-speed rotor, replaceable hammers, wear-resistant liner plates and a bottom screen grate to reduce rigid and irregular cast aluminum parts into smaller pieces. The screen opening helps control the maximum discharge size for collection, transportation, furnace feeding or downstream ferrous removal.
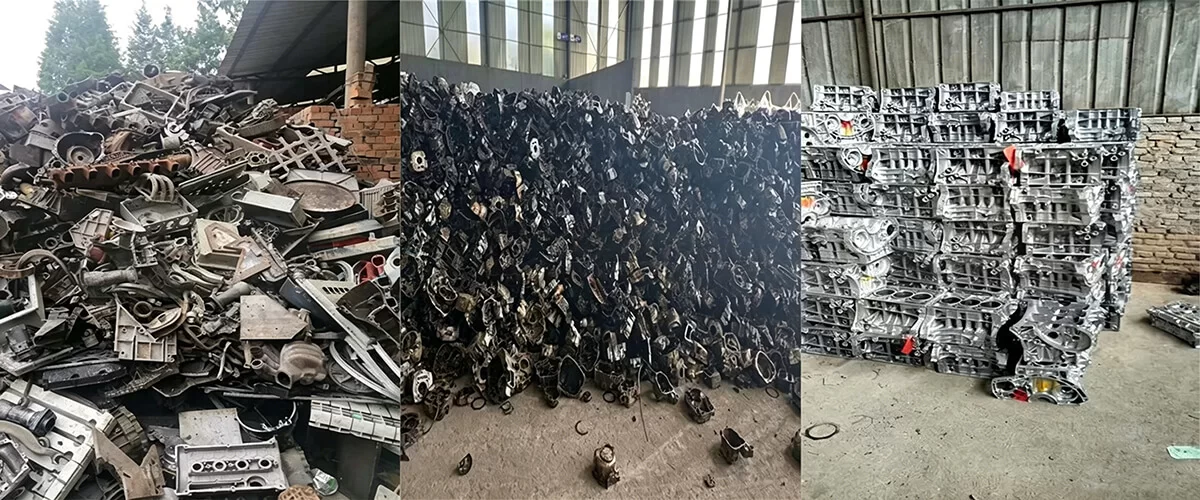
Cast Aluminum Parts Suitable for Crushing
The machine is intended for identified and prepared cast aluminum parts rather than unsorted mixed aluminum scrap. Typical materials include:
Broken cast aluminum components
Dismantled cast aluminum housings
Rejected die-cast aluminum parts
Cast machinery components
Hollow cast aluminum enclosures
Thick aluminum casting offcuts
Prepared cast parts containing removable steel attachments
Material suitability depends on the maximum part dimensions, wall thickness, individual weight, internal structure and remaining ferrous components. The crusher model should be selected from representative material information rather than the material name alone.
Preparation Before Crushing
Cast aluminum parts should be inspected before feeding. Residual oil, coolant and other free liquids must be drained. Sealed cavities should be opened or evaluated separately.
Large steel shafts, gears, bearings, tools and thick structural inserts should be removed where practical. Small screws, brackets and limited steel inserts may remain only when their dimensions and quantity are within the operating limits of the selected crusher.
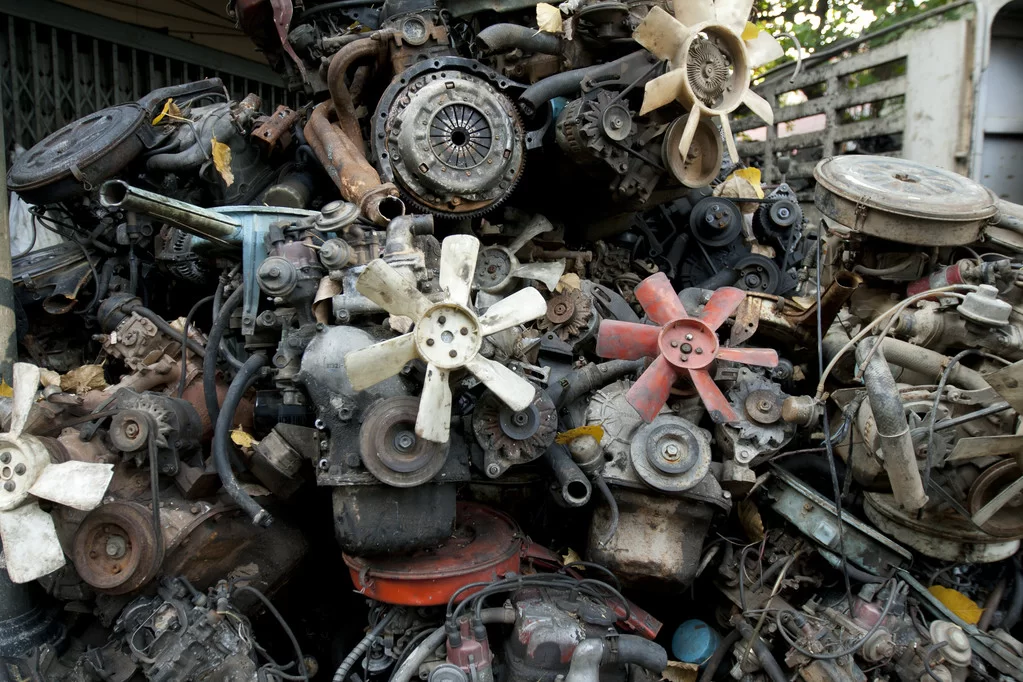
Complete engines and transmissions should not be treated as prepared cast aluminum parts. These assemblies normally contain large steel shafts, gears, bearings, fluids and other components that require dismantling before crushing.
Hammer Crushing and Screen-Controlled Output
The high-speed rotor drives the hammers to repeatedly impact and break the cast aluminum inside the crushing chamber. The rigid casting structure is reduced through impact, bending and compression between the hammers, liner plates and screen grate.
Material remains inside the chamber until sufficiently reduced pieces pass through the selected screen openings. The screen controls the maximum discharge size but does not produce pieces with identical dimensions.
The actual output distribution depends on the casting wall thickness, internal ribs, part shape, hammer arrangement, screen opening and feeding condition.
Individual Machine Positioning
The cast aluminum parts crusher can operate as an individual machine with suitable feeding and discharge connections. It performs high-speed hammer crushing and should not be confused with a low-speed twin shaft shredder.
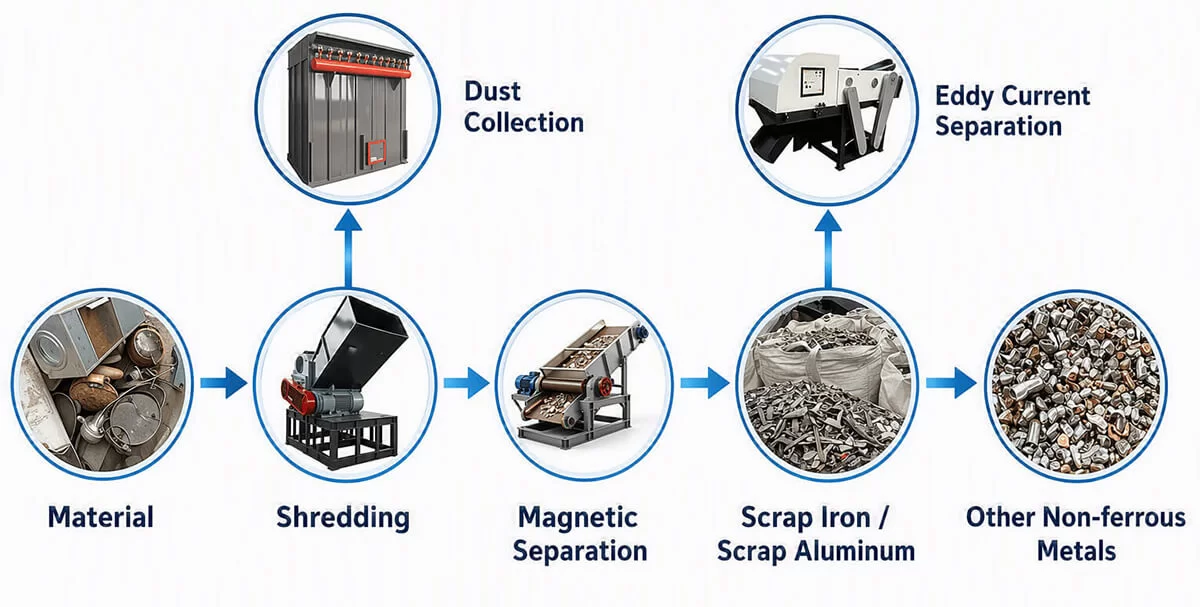
Oversized or difficult-to-feed parts may require dismantling, hydraulic breaking or primary shredding before entering the crusher. When exposed ferrous attachments must be removed after crushing, a magnetic separator can be selected as separate downstream equipment.
Materials Covered by Other Equipment
Aluminum alloy wheels, long aluminum profiles, mixed recycling-yard aluminum, aluminum turnings, sealed containers, aluminum dross and aluminum ash are not the primary materials covered by this page. These materials have different feeding, crushing or safety requirements and should be evaluated separately.
Prepared Cast Aluminum Parts Covered by This Page
This application is intended for a comparatively consistent stream of sorted cast aluminum parts with known dimensions and wall thickness. Typical feed may include prepared valve bodies, pump housings, machinery covers, brackets, small industrial housings and other identifiable cast parts that fit the selected crusher opening.
Mixed foundry scrap containing sprues, runners, irregular offcuts and castings with widely different dimensions should be evaluated as general cast aluminum crusher feed. Complete engines, crankcases and transmission assemblies belong to the dedicated crankcase processing pages because their steel shafts, gears, bearings and fluids require separate assessment.
Consistency Requirements Before Continuous Feeding
Confirm the maximum dimensions, weight range, wall thickness, steel inserts and hourly feed rate. A more consistent feed improves loading stability and makes screen, hammer and conveyor selection more reliable. Oversized parts, sealed cavities and heavy steel attachments must be removed, dismantled or tested separately.