An eddy current separator is often described as a machine for separating aluminum and other non-ferrous metals. That description is correct, but it does not explain why two machines with a similar belt width can produce very different results.
In an actual recycling line, separation performance depends on the condition of the material before it reaches the separator. Particle size, moisture, iron content, feeding thickness and belt speed can all affect the final recovery rate. For this reason, choosing an eddy current separator should start with the material, not simply with the motor power or equipment dimensions.
What Does an Eddy Current Separator Remove?
An eddy current separator is used to recover conductive non-ferrous metals from a mixed material stream. Typical recoverable materials include:
Aluminum pieces
Copper fragments
Brass particles
Aluminum alloy scrap
Non-ferrous metal from automotive shredder residue
Aluminum recovered from household appliance scrap
Metal fragments from mixed industrial waste
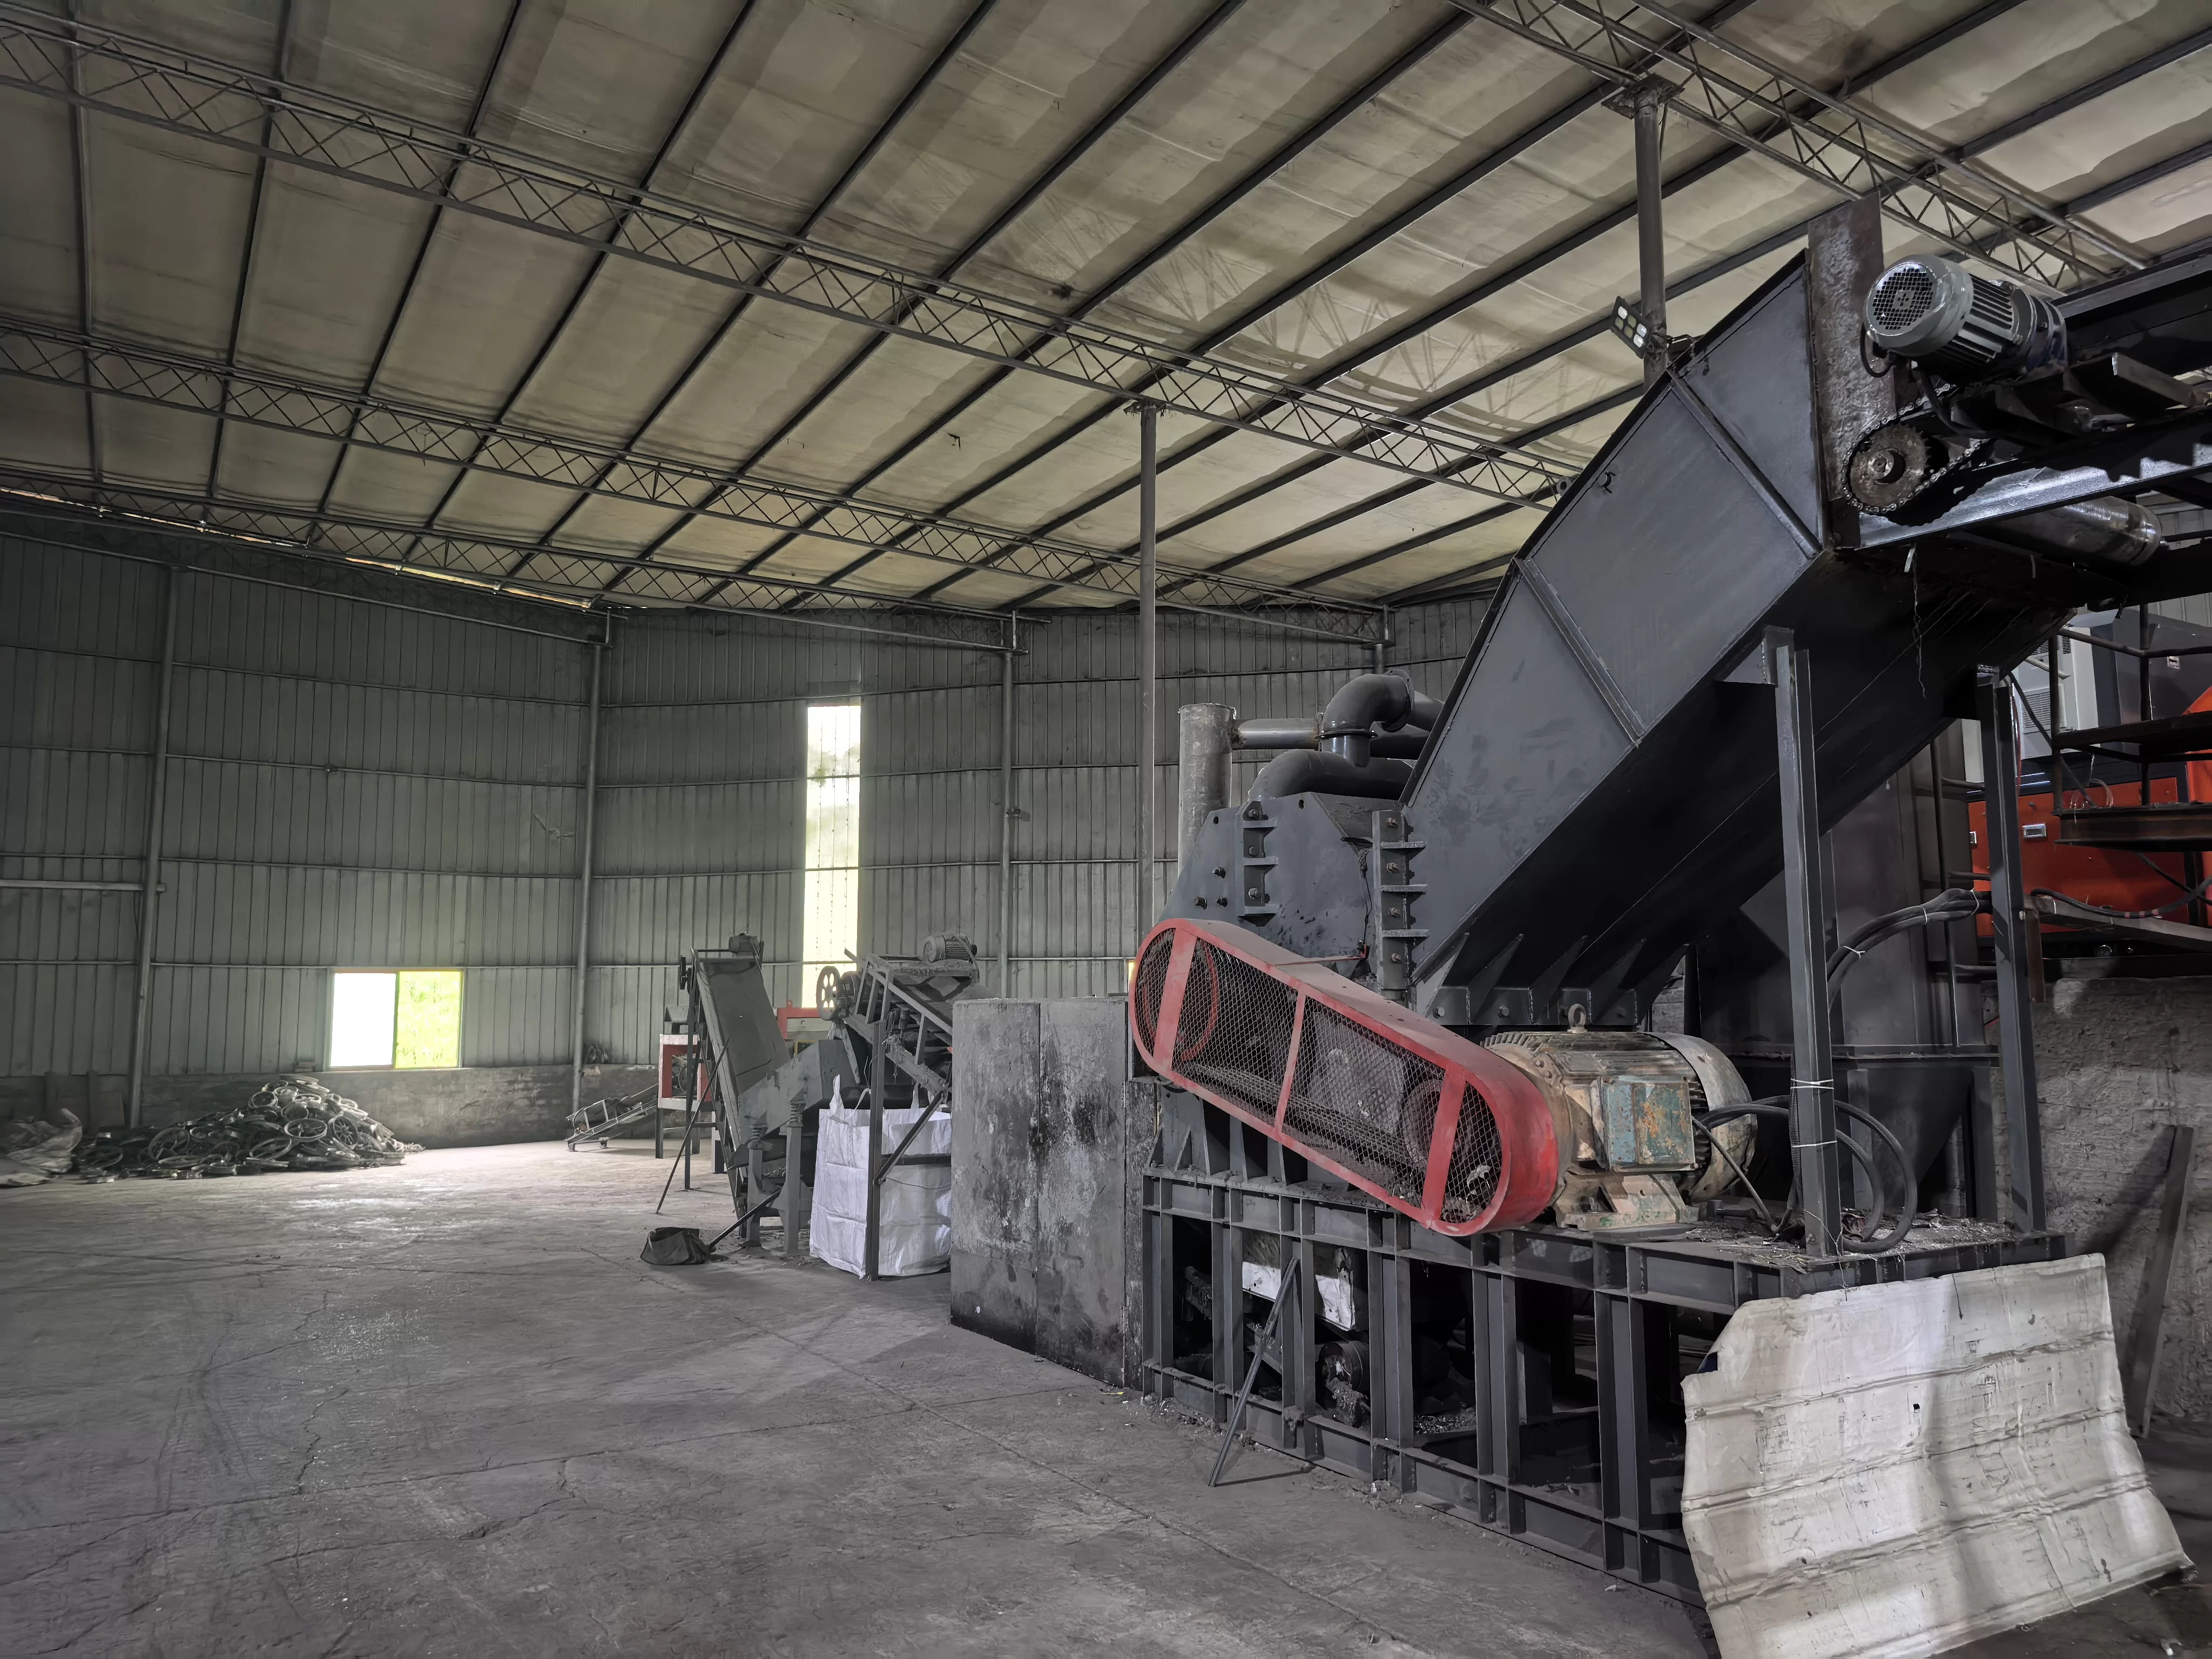
The machine is normally installed after size reduction and ferrous metal removal. A crusher or shredder reduces the feed material to a more manageable size, while a magnetic separator removes most iron and steel before the remaining material enters the eddy current separator.
This sequence matters. If a large amount of ferrous metal reaches the high-speed magnetic rotor, it can reduce separation stability and increase the risk of equipment damage.
Particle Size Has a Direct Effect on Separation
Consistent particle size generally produces a more stable separation result. When the feed contains a mixture of very large pieces and fine powder, each fraction responds differently as it leaves the belt.
Large pieces have greater mass and may require a stronger magnetic response to follow the desired trajectory. Very fine particles can be affected by dust, vibration and neighboring materials. Flat aluminum pieces may also behave differently from dense cast aluminum of the same apparent size.
Before selecting a separator, the buyer should provide a realistic particle size range rather than only an average value. Useful information includes:
Minimum particle size
Maximum particle size
Percentage of material below 10 mm
Typical shape of aluminum pieces
Approximate bulk density
Required purity after separation
If the size range is too wide, a vibrating screen can divide the feed into separate fractions before eddy current separation. In many projects, improving material classification gives a better result than simply increasing rotor speed.
Stable Feeding Is More Important Than a Thick Material Layer
An eddy current separator needs an even, single-layer feed as far as possible. When material forms a thick bed on the belt, aluminum or copper pieces can become trapped under plastic, rubber or stainless steel.
A wider belt does not automatically mean higher effective capacity. The feeding conveyor, vibrating feeder and distribution system must spread the material across the working width.
Operators should pay attention to:
Uneven loading on one side of the belt
Sudden surges from the upstream conveyor
Large pieces covering smaller valuable metals
Wet material sticking together
Long wires or strips becoming entangled
If the upstream crusher discharges material unevenly, adding a buffer bin or controlled vibrating feeder may improve separator performance more than replacing the separator itself.
Belt Width Should Match the Actual Processing Capacity
Belt width helps determine how much material can be distributed across the separation zone, but capacity also depends on bulk density and feed thickness.
For example, one ton of dense aluminum casting fragments occupies much less volume than one ton of light sheet aluminum. A separator selected only by tons per hour may therefore be too narrow for low-density, bulky material.
The supplier should know:
Required capacity per hour
Loose bulk density of the feed
Maximum particle size
Percentage of non-ferrous metal
Available installation space
Upstream conveyor discharge width
A suitable separator should handle the required volume without forcing the operator to create an excessively thick layer.
Rotor Speed Must Be Matched to the Material
The magnetic rotor creates a rapidly changing magnetic field. Conductive metal passing through this field develops eddy currents and is projected away from the normal material trajectory.
Higher rotor speed can improve the response of some small or light aluminum particles, but maximum speed is not always the best setting. Excessive speed may make the discharge trajectory unstable, especially when the material has a wide size distribution.
A variable-frequency control system is useful because it allows the operator to adjust:
Magnetic rotor speed
Conveyor belt speed
Feeding rate
Discharge splitter position
The correct settings are normally found through a material test. A test should use the customer’s regular production material, not a small quantity of clean aluminum prepared only for demonstration.
Moisture and Dust Can Reduce Sorting Stability
Dry and loose material usually separates more consistently than wet or oily material. Moisture can cause fine particles to stick to larger pieces, while oil can make the belt surface dirty and affect material movement.
Dust is another operational issue. Fine powder can enter bearings, accumulate around the belt and make daily inspection more difficult.
Depending on the material, the complete line may require:
Dust collection
Belt cleaning
Sealed transfer points
Regular rotor-area inspection
Screening before separation
Drying or drainage before feeding
These supporting systems should be considered during line design rather than added only after separation problems appear.
Do Not Judge Performance by Aluminum Recovery Alone
A separator may recover a high percentage of aluminum but still produce a contaminated product. Recovery and purity should therefore be evaluated together.
A practical material test should measure:
Aluminum recovery rate
Purity of the recovered fraction
Valuable metal remaining in the waste fraction
Material loss caused by incorrect splitter position
Output stability during continuous feeding
If purity is more important than one-pass recovery, the plant may use two-stage separation. The first separator recovers the main aluminum fraction, while a second pass cleans the product or recovers remaining valuable metal.
Information to Send Before Requesting a Quotation
To receive a useful equipment recommendation, send the supplier the following information:
Clear photos and videos of the mixed material
Material source
Particle size range
Moisture and oil condition
Iron content before separation
Estimated aluminum and copper percentage
Required hourly capacity
Required final purity
Existing crusher, screen and magnetic separator details
Local voltage and frequency
Plant layout or available installation dimensions
A representative material sample is especially useful. Separation videos can provide an initial reference, but an actual test gives more reliable information about trajectory, purity and product loss.
Final Selection Advice
Choosing an eddy current separator is not only a matter of comparing magnetic strength or belt width. The complete process must provide a controlled particle size, remove ferrous metal and distribute the feed evenly.
When the upstream process is stable, the separator can be adjusted for better recovery and purity. When the feed is poorly prepared, even a larger machine may not solve the problem.
Haoxing Machinery can configure crushing, screening, magnetic separation and eddy current separation equipment according to the customer’s material condition and required capacity. Before requesting a solution, prepare material photos, particle size data, hourly output and final purity requirements. This information helps the engineering team recommend a more practical recycling line.