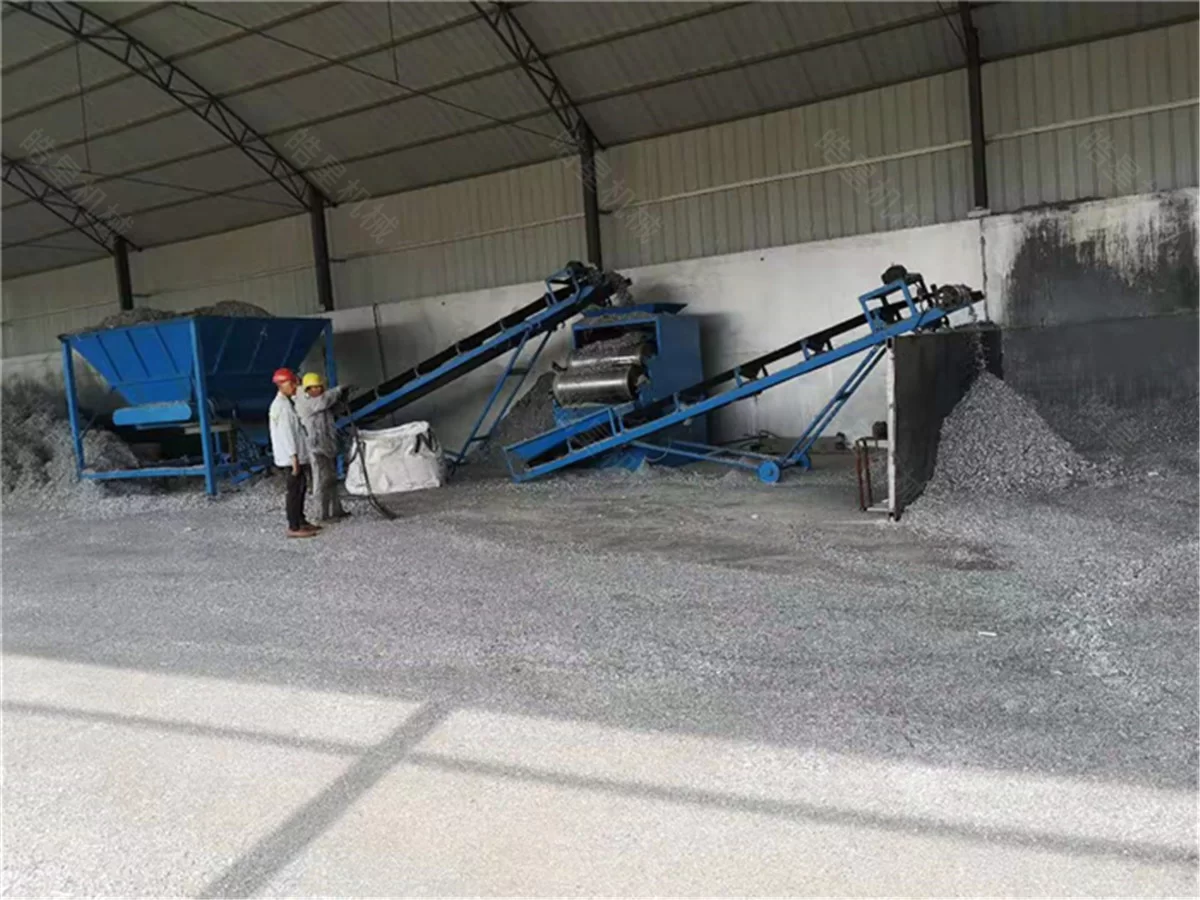
Long, curled metal turnings can occupy a surprisingly large amount of storage space. The problem is often most noticeable with aluminum and steel turnings that become tangled during machining. A container may look full even though the actual metal weight inside it is relatively low.
Crushing shortens the turnings and breaks apart tangled chip nests. The processed material normally settles more evenly, making it easier to convey, store or feed into downstream equipment. However, volume reduction should not be judged from photographs alone.
A useful test requires equal-weight samples, the same measuring container and a consistent filling method.
What Does Volume Reduction Mean?
Volume reduction describes the change in the space occupied by a known quantity of material before and after processing.
For metal turnings, the comparison is usually affected by two changes:
Long chips are shortened.
Tangled chip nests are opened and separated.
These changes allow the processed material to occupy the available container space more efficiently.
Volume reduction is not the same as weight reduction. Crushing changes the form of the turnings, but it should not significantly change the amount of metal present, apart from removed liquids, contaminants or processing losses.
This distinction becomes important when wet machining chips are tested. If coolant or oil is removed during the process, the final sample may weigh less than the original sample. A direct volume comparison would then be misleading unless the liquid loss is recorded separately.
Why Photographs Are Not Enough
Before-and-after photographs can show that the chip shape has changed, but they do not provide a reliable volume reduction result.
A photograph may be influenced by:
Different sample weights
Different containers
Camera angle
Manual compression of one sample
Uneven filling
Different oil or coolant content
Material settling during storage
Solid pieces mixed with the turnings
For example, a container filled with loosely dropped original turnings should not be compared with a second container in which the crushed chips have been shaken or compressed.
A visual comparison is useful for showing chip condition. A measured comparison is needed for evaluating storage and material-handling performance.
Use Equal-Weight Samples
The simplest test starts with two samples of the same metal weight.
One sample remains in its original condition. The other sample is processed by the turnings crusher. Both samples are then placed into the same calibrated container under controlled filling conditions.
The basic test sequence is:
Prepare a representative batch of metal turnings.
Remove foreign objects that are not part of the normal feed.
Record the initial liquid condition.
Weigh the original sample.
Measure the volume occupied by the original sample.
Process the sample through the crusher.
Collect all discharged material.
Weigh the processed material again.
Measure the volume occupied by the processed material.
Record any recovered liquid, fine material or residue.
The original and processed sample weights should be as close as practical. If the weights differ, the result should be normalized before a direct comparison is made.
Choose a Suitable Measuring Container
The container should have a known internal volume or clearly marked volume graduations.
A straight-sided container is easier to use than a container with a tapered or irregular shape. The container should also be large enough to hold a representative quantity of turnings.
Possible test containers include:
A calibrated steel box
A straight-sided plastic container
A drum with verified internal dimensions
A rectangular test bin
A weighed bulk bag with a measured filling frame
Very small samples can give inconsistent results because one large chip nest may occupy a considerable part of the container. A larger representative sample normally provides a more useful indication of actual storage behavior.
The following container information should be recorded:
Internal length
Internal width
Internal height
Total internal volume
Empty container weight
Measuring graduations, if used
The same container should be used for both measurements.
Keep the Filling Method Consistent
The way metal turnings enter the container affects the measured volume.
The test should state whether the material is:
Poured directly into the container
Dropped through a chute
Fed by a conveyor
Placed manually
Vibrated after filling
Compressed or left loose
For a basic comparison, both samples can be allowed to fall naturally into the container without manual pressing.
If the actual production system uses a vibrating hopper or settling conveyor, a second test may be carried out using controlled vibration. The original and crushed samples must still receive the same treatment.
Do not push down only the processed chips to make the volume reduction appear greater. The purpose of the test is to reproduce normal storage or conveying conditions.
Measuring the Original Volume
Long metal turnings often form irregular surfaces inside a container. The top of the sample may not be level, so the occupied volume cannot always be read from a single point.
For a rectangular container, measure the material height at several positions and calculate an average filling height.
The occupied volume can then be estimated as:
Occupied volume = Container length × Container width × Average material height
If the container has volume markings, record the closest practical reading without pressing the chips below the marked level.
The test report should include a photograph of the filled container and the measuring points used. This makes the result easier to understand and repeat.
Measuring the Crushed Volume
After crushing, collect the processed chips without intentionally removing acceptable material.
Before measuring the volume, check for:
Material remaining inside the crusher
Chips left on the conveyor
Oversized pieces returned for further processing
Fine material collected separately
Oil or coolant leakage
Foreign objects removed during the test
Weigh the collected material. If the final weight is close to the original weight, fill the same test container using the same method.
Record the average material height or indicated container volume. The difference between the two occupied volumes can then be calculated.
Volume Reduction Calculation
The volume reduction rate can be calculated using:
Volume reduction rate = (Original volume − Crushed volume) ÷ Original volume × 100%
For example, suppose an equal-weight sample occupies 1.0 cubic metre before crushing and 0.4 cubic metre after crushing.
The calculation is:
(1.0 − 0.4) ÷ 1.0 × 100% = 60%
This example only demonstrates the calculation method. It is not a guaranteed result for a particular machine or material.
The actual reduction depends on the original chip shape, nest size, metal type, crushing condition and filling method.
Bulk Density Provides Another Useful Measurement
Bulk density describes the mass of material contained in a known volume.
It can be calculated as:
Bulk density = Sample weight ÷ Occupied volume
If the sample weight remains unchanged while the occupied volume decreases, the measured bulk density increases.
Bulk density is useful when planning:
Storage-bin capacity
Conveyor loading
Container utilization
Briquetting feed
Furnace charging
Material transport
The report should clearly state whether the material was loose-filled, settled, vibrated or compressed. Bulk density measured under one condition should not be presented as though it applies to every handling system.
Account for Oil and Coolant
Machining turnings may contain cutting oil, emulsion or coolant.
Liquid content affects both sample weight and chip behavior. Wet turnings may stick together, while free liquid can collect at the bottom of the measuring container.
Before testing, record:
Liquid type
Approximate liquid content
Whether free liquid is present
Whether the process includes drainage or centrifuging
Whether the final weight refers to wet or dry metal
If crushing and liquid separation take place in the same test, the report should show a simple material balance:
Wet turnings entering the process
Processed metal chips collected
Liquid recovered
Fine material collected
Residue remaining in the equipment
Without this information, part of the apparent volume change may come from liquid removal rather than chip-size reduction.
Different Turnings Produce Different Results
Metal type alone does not determine the result. Chip form is equally important.
Aluminum Turnings
Aluminum turnings may be soft, flexible and easily tangled. Long aluminum chips can form large nests with low loose bulk density.
Shortening these chips can improve hopper flow and reduce bridging. Excessive crushing should still be avoided because repeated cutting may produce more fines and increase the exposed metal surface.
Steel Turnings
Steel turnings may form strong spiral or spring-like shapes. Large nests can be difficult to separate manually and may not feed steadily into a briquetting press or storage hopper.
The crusher must provide sufficient cutting action without being designed around only the easiest short chips.
Cast Iron Chips
Cast iron chips are often shorter and more brittle than long steel or aluminum turnings. Their initial bulk density may already be higher, so the volume change after crushing may be less dramatic.
Dust and fine-particle control can be more important when processing brittle material.
Mixed Turnings
Mixed loads may contain long chips, short chips, solid offcuts and contaminants. A single volume reduction figure can hide these differences.
Where practical, different chip types should be tested separately before evaluating the mixed feed.
Why Over-Crushing Should Be Avoided
A larger volume reduction figure does not automatically indicate a better process.
Breaking the metal into excessively small pieces may result in:
More metal fines
Higher dust levels
Increased power consumption
Faster cutter wear
Greater material loss during handling
More exposed surface area
Increased oxidation during storage or melting
Difficulties in recovering fine chips from coolant
The required output should be based on the next processing stage.
If the chips only need to flow steadily into a briquetting press, they do not need to be reduced to powder. If the chips will be charged into a furnace, excessive fines may also create handling and recovery problems.
The target is controlled chip shortening, not maximum breakage.
Check the Oversize Fraction
Volume measurement alone does not show whether the processed material is suitable for downstream use.
After crushing, inspect the sample for long or tangled pieces that remain in the product. These pieces may still bridge inside a conveyor, storage bin or briquetting feed hopper.
A practical test should record:
Maximum chip length
Typical chip length
Remaining tangled nests
Oversized fraction
Fine-particle fraction
Presence of solid offcuts
Where necessary, a screen can separate material that requires another processing pass. However, the screen opening and return system should be selected according to the final feeding requirement.
Measure the Actual Production Result
A short demonstration using a small, carefully selected sample may not represent continuous operation.
For a more useful production test, record:
Total feed weight
Test duration
Actual processed output
Original occupied volume
Final occupied volume
Number of feeding interruptions
Crusher reversing or blockage events
Oversized material returned
Fine material collected
Liquid recovered
Material remaining in the equipment
The test feed should include the normal variation found in production. Removing all difficult nests or longer chips before the test can make the result unrealistic.
How Volume Reduction Affects Storage
Shortened turnings can use storage space more efficiently, but the storage system must still allow the material to discharge reliably.
A higher bulk density may reduce the required bin volume for a given metal weight. It may also increase the load on:
Bin walls
Supporting structures
Discharge screws
Conveyor belts
Transfer chutes
Storage equipment should therefore be checked by weight as well as by volume.
A container that holds more processed metal may exceed its permitted transport weight before it reaches its full physical volume.
How Volume Reduction Affects Transportation
Loose, tangled turnings can fill a truck body, container or bulk bag before reaching the allowable payload.
Reducing the occupied volume may allow more metal to be moved in each load. The actual benefit depends on:
Legal transport weight
Container payload
Loading method
Remaining liquid content
Final chip bulk density
Packaging requirements
Restrictions on loose metal fines
Transportation planning should compare both available volume and permitted weight. A denser load is only useful when it remains within the legal and structural limits of the transport equipment.
How Volume Reduction Affects Briquetting
Long turnings can bridge across a hopper and interrupt the flow into a briquetting press. Shorter chips usually provide a more consistent feed condition.
However, volume reduction alone does not prove that the material is ready for briquetting.
The processed chips should also be evaluated for:
Maximum length
Flow through the feed hopper
Remaining coolant content
Fine-particle percentage
Consistency of metering
Presence of solid metal pieces
A briquetting trial using the processed chips is the most direct way to confirm whether the preparation stage is suitable.
Information Required Before Testing
Before selecting a crushing process or arranging a material test, provide:
Metal type and grade
Photographs of loose turnings
Photographs of tangled chip nests
Maximum chip length
Approximate nest dimensions
Original loose bulk density, if available
Oil or coolant type
Approximate liquid content
Required processing capacity
Downstream storage or conveying method
Briquetting or furnace feed requirements
Acceptable fine-particle level
A representative sample is particularly important when the feed contains several chip forms.
Recommended Test Report
A useful report should contain:
Material description
Sample photographs
Original sample weight
Crushed sample weight
Original occupied volume
Crushed occupied volume
Filling method
Container dimensions
Calculated bulk densities
Calculated volume reduction
Liquid recovery
Oversize observations
Fine-material observations
Test duration
Actual throughput
Photographs of the final product
These details allow the result to be reviewed later and compared with future tests.
Conclusion
The volume reduction of metal turnings should be measured with equal-weight samples, the same calibrated container and a consistent filling method. Photographs can show changes in chip form, but they cannot replace weight and volume measurements.
The most useful result is not necessarily the largest reduction percentage. The processed chips must also be suitable for storage, conveying, liquid separation, briquetting or furnace charging.
A representative material test should record the original chip condition, occupied volume, processed volume, weight balance, liquid content and final chip form. This provides a more reliable basis for selecting a turnings crusher and designing the downstream handling system.